Reasons for choosing our testing services
ZHONGXI Testing has obtained inspection qualification certifications from multiple countries and regions worldwide. We possess a senior testing team and advanced testing methods, providing independent, impartial, and professional third-party verification services for global carbon projects.
Internationally recognized authority
Certified by multiple international standards such as CNAS, VCS, and GS, with reports universally applicable worldwide.
Global service capability
Covering 140+ countries and regions, it supports on-site detection and remote verification in multiple languages.
Professional experimental methods
Adopt standard experimental methods to ensure accurate and reliable data.
Comprehensive Characterization and Performance Assessment of Attapulgite Clay Desiccants – Specialized Analytical Services
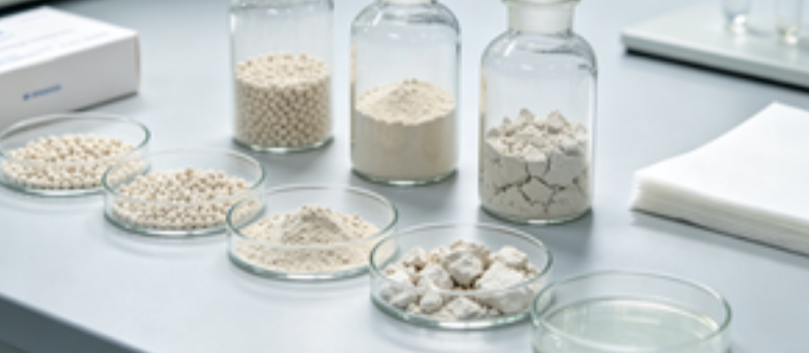
Attapulgite (also known as palygorskite) clay is a naturally occurring hydrated magnesium aluminium silicate with a unique fibrous morphology and a microporous channel structure. These intrinsic properties confer exceptional moisture adsorption capacity, making attapulgite a widely used desiccant in packaging, electronics, pharmaceuticals, and industrial drying applications. However, the performance and reliability of attapulgite-based desiccants are governed by a complex interplay of mineralogical purity, specific surface area, pore architecture, surface acidity, cation exchange capacity, thermal stability, and moisture uptake kinetics. If you are seeking testing services for attapulgite clay desiccants, you are likely at a point where accurate, multi-dimensional characterisation is essential to verify raw material quality, optimise activation and granulation processes, ensure batch-to-batch consistency, or diagnose premature saturation and performance loss in service. This article details our comprehensive analytical and performance testing platform, the scientific depth we bring, and the distinct advantages that make us a trusted partner for desiccant manufacturers, industrial hygiene laboratories, and quality assurance departments worldwide.
The Scientific Imperative for Holistic Attapulgite Desiccant Testing
The moisture adsorption behaviour of attapulgite is governed by a combination of physical adsorption (onto the external surface and within the zeolite-like channels) and chemisorption (via surface hydroxyl groups and exchangeable cations). The equilibrium moisture capacity and adsorption rate are critically dependent on the specific surface area (BET), the micro- and mesopore volume distribution, the surface polarity, and the presence of impurities such as carbonates, quartz, or other clay minerals. Furthermore, the desiccant's performance under varying temperature and relative humidity, its regenerability, and its mechanical integrity during handling and packaging are equally important for industrial applications. A single test, such as moisture content or bulk density, cannot capture these complexities. Therefore, a systematic testing strategy that integrates mineralogical, physicochemical, textural, and dynamic adsorption characterisation is indispensable. Our service is architected to provide this integrated insight, enabling you to correlate processing parameters with performance and to troubleshoot field failures effectively.
Our Comprehensive Analytical and Performance Testing Capabilities for Attapulgite Desiccants
We deploy a broad suite of complementary techniques, each optimised to address a specific aspect of attapulgite desiccant characterisation—from bulk mineralogy to real-time moisture uptake under simulated service conditions.
1. Mineralogical and Chemical Composition: We perform X‑ray diffraction (XRD) with Rietveld refinement to identify the crystalline phases, quantify the attapulgite content, and detect impurities such as quartz, calcite, dolomite, or sepiolite. X‑ray fluorescence (XRF) and inductively coupled plasma optical emission spectrometry (ICP‑OES) provide the bulk elemental composition (Si, Al, Mg, Fe, Ca, Na, K, etc.), which is essential for assessing purity and for predicting cation exchange behaviour. Thermogravimetric Analysis (TGA) coupled with evolved gas analysis (MS or FTIR) measures the loss of hygroscopic water, zeolitic water, and structural hydroxyl groups, providing insight into thermal stability and the temperature range for effective regeneration.
2. Textural Properties – Surface Area and Porosity: The moisture adsorption capacity is directly linked to the specific surface area and pore structure. We determine BET specific surface area using nitrogen or argon physisorption at 77 K or 87 K, with full pore-size distribution (DFT/BJH models) covering micropores and mesopores. For materials with significant microporosity, we also perform CO2 adsorption at 273 K to characterise the ultramicropore region (< 0.7 nm). Mercury intrusion porosimetry is used to assess macroporosity and interparticle void space in granulated or pelletised desiccants, which affects the kinetics of moisture uptake.
3. Surface Chemistry and Cation Exchange Capacity (CEC): The surface acidity and the presence of exchangeable cations (Na+, K+, Ca2+, Mg2+) strongly influence water adsorption affinity. We measure cation exchange capacity by the ammonium acetate method (pH 7) and determine the point of zero charge (pHPZC) by potentiometric titration or salt addition. X‑ray photoelectron spectroscopy (XPS) provides the surface elemental ratios and the chemical states of Si, Al, Mg, and O, revealing the degree of isomorphous substitution and the nature of surface hydroxyl groups. Fourier‑transform infrared spectroscopy (FTIR) in diffuse reflectance (DRIFTS) mode identifies the characteristic bands of structural OH, Si–O–Si, and Al–OH, and can detect any organic contaminants or adsorbed species.
4. Moisture Adsorption Equilibrium and Kinetics: We conduct static gravimetric adsorption tests at controlled relative humidities (5–90% RH) and temperatures (20–50 °C) using saturated salt solutions or automated vapour sorption analysers. We obtain water adsorption isotherms and fit them to models (e.g., BET, GAB, or Langmuir) to determine the monolayer capacity and the heat of adsorption. Dynamic water vapour sorption (DVS) measurements provide real-time kinetics, allowing us to calculate diffusion coefficients and identify the rate-limiting step (film diffusion vs. pore diffusion). We also evaluate the desorption behaviour to assess regenerability and hysteresis.
5. Dynamic Moisture Uptake in Simulated Service Conditions: For practical applications, we use a custom-built flow-through test rig that exposes the desiccant to a controlled stream of air with defined temperature, relative humidity, and flow rate. We measure the breakthrough time and the dynamic capacity up to a specified endpoint (e.g., 10% relative humidity outlet). This simulates real-world packaging or storage scenarios and provides direct performance metrics for quality control.
6. Mechanical Strength and Attrition Resistance: For granular or pelletised desiccants, mechanical robustness is critical. We perform crush strength testing (individual pellets) and attrition tests (ASTM D4058 or similar) to quantify the resistance to particle breakage during handling, transportation, and use. We also measure bulk density and tap density, which affect packaging and fill volume.
7. Regenerability and Cyclic Stability: The economic viability of a desiccant depends on its ability to be regenerated multiple times. We subject the material to repeated adsorption–desorption cycles under controlled conditions (e.g., heating at 150–250 °C under vacuum or dry air purge). After each cycle, we measure the residual moisture capacity and characterise the material by XRD, BET, and FTIR to detect any structural degradation, phase changes, or loss of active sites.
8. Leaching and Contaminant Testing: For desiccants used in food or pharmaceutical packaging, safety is paramount. We perform leaching tests according to relevant regulatory guidelines (e.g., USP, FDA) by extracting the desiccant with water or acidic solution and analysing the eluate by ICP‑MS (for heavy metals such as Pb, Cd, As, Hg) and ion chromatography (for anions like fluoride, chloride). We also test for dust generation and particulate release to comply with cleanroom standards.
9. Advanced Spectroscopic and Imaging Analysis: For detailed microstructural investigation, we offer high-resolution transmission electron microscopy (HR-TEM) to visualise the fibrous morphology and the presence of amorphous or crystalline coatings. Electron paramagnetic resonance (EPR) can detect paramagnetic impurities (e.g., Fe3+) that may affect adsorption behaviour. Solid-state 29Si and 27Al MAS‑NMR provides atomic-level information on the coordination of silicon and aluminium, revealing the structural ordering and the degree of tetrahedral/octahedral substitution.
Advanced Diagnostics – Beyond Routine Desiccant Testing
Our service goes beyond standard isotherms and breakthrough tests. We integrate experimental data with mathematical modelling to predict desiccant performance under variable conditions, such as fluctuating temperature and humidity. We also develop accelerated aging protocols to simulate long-term storage or extended service, providing you with reliable lifetime predictions. For research and development, we offer in-situ XRD or in-situ FTIR during moisture adsorption to monitor structural changes and hydration/dehydration mechanisms in real time. Our chemometric analysis can correlate multiple characterisation parameters to optimise activation conditions and improve batch consistency.
Our Distinctive Advantages in Attapulgite Desiccant Testing
Our laboratory has decades of combined experience in clay mineralogy and industrial desiccant evaluation. We offer several unique strengths that set us apart:
Advantage 1 – Fully Integrated Multi-Technique Platform: We house all essential instruments—XRD, XRF, ICP, BET, TGA-MS, FTIR, DVS, flow-through test rigs, mechanical testers, and ICP-MS—under one ISO/IEC 17025‑accredited roof. This eliminates outsourcing delays, reduces cross‑contamination risks, and allows seamless correlation of structural, chemical, and performance data from the same sample batch.
Advantage 2 – Tailored Protocols for Diverse Attapulgite Grades: Attapulgite sources differ in fibre length, purity, and associated minerals. We customise degassing, activation, and testing conditions (e.g., temperature, humidity, gas composition) to your specific material, ensuring that measurements reflect true intrinsic properties and that performance tests mirror your target application.
Advantage 3 – Unrivalled Depth in Mineralogical and Surface Characterisation: Our combination of Rietveld XRD, XPS, and solid‑state NMR allows us to quantify not only the major phases but also subtle substitutions and defect structures that directly influence adsorption affinity. We can distinguish between structural and adsorbed water with high precision.
Advantage 4 – Realistic Dynamic Performance Evaluation: Our flow‑through rigs simulate actual packaging or industrial drying conditions, including cyclic changes in humidity and temperature. This provides you with directly applicable performance data, such as time to reach a given dew point, which standard static tests cannot deliver.
Advantage 5 – Comprehensive Quality Assurance and Regulatory Support: We can test according to international standards (ASTM, ISO, USP, FDA) and provide full validation reports for regulatory submissions. Our data are traceable and defensible, giving you confidence in audits and product certifications.
Advantage 6 – Rapid Turnaround with Dedicated Project Management: Most projects are completed within 10–14 working days, with expedited services for urgent troubleshooting. You are assigned a dedicated project scientist who communicates progress regularly, shares preliminary data, and adjusts the test plan based on your feedback.
Advantage 7 – Global Logistics and Strict Confidentiality: With sample intake hubs in North America, Europe, and Asia‑Pacific, we facilitate seamless international shipping. Our secure online portal ensures data protection and instant access to final reports (PDF, Excel, raw data). We are pleased to sign non‑disclosure agreements to safeguard your proprietary information.
Who Benefits from Our Services
Our testing solutions are tailored for a broad spectrum of stakeholders: attapulgite mining and processing companies seeking quality control and product optimisation; desiccant manufacturers needing performance certification and batch‑to‑batch consistency; packaging and electronics industries evaluating desiccants for moisture‑sensitive products; pharmaceutical and food companies requiring safety and efficacy verification; and regulatory and certification bodies requiring independent testing for compliance.
Performance Benchmarks and Technical Specifications
To illustrate the precision of our measurements, we highlight typical performance indicators:
- BET surface area precision: ± 0.3 m²/g for reference materials.
- XRD phase quantification: ± 0.5 wt% for major phases.
- Water adsorption isotherm repeatability: ± 0.5% relative uptake at 50% RH.
- Dynamic breakthrough capacity: RSD ≤ 2% for identical runs.
- Crush strength precision: ± 1 N for pelletised samples.
- ICP‑MS detection limits: < 0.1 ppb for heavy metals.
- TGA mass loss accuracy: ± 0.02 mg.
- FTIR spectral resolution: 2 cm−1, enabling clear identification of OH and Si–O bands.
These capabilities ensure that even subtle differences—such as a 2% variation in microporosity or a 1% shift in equilibrium capacity—are reliably detected and statistically valid.
How to Initiate a Testing Project
Engaging our service is simple and efficient. It begins with a complimentary consultation where we discuss your attapulgite desiccant (source, activation process, intended application), your specific objectives (e.g., incoming material verification, performance benchmarking, trouble‑shooting), and any regulatory requirements. We then propose a customised testing matrix with transparent cost estimates and a clear timeline. After your approval, we provide detailed sample submission guidelines (quantity, packaging, handling). Upon receipt, we perform an initial quality check and then launch the full analytical workflow. You will receive regular progress updates, and at the conclusion, a comprehensive final report integrating all results, statistical analysis, and expert interpretation, followed by an optional debriefing session.
Quality Assurance and Ethical Standards
Our laboratory operates under ISO 9001 and ISO/IEC 17025:2017 accreditation. All data are recorded in electronic laboratory notebooks with full audit trails. We follow stringent safety protocols for handling clay minerals and chemicals. We are committed to unbiased, transparent reporting and to the highest level of confidentiality for your proprietary materials and data.
Conclusion – Ensure Optimal Performance and Reliability of Your Attapulgite Desiccants
Attapulgite clay desiccants offer a cost-effective and efficient solution for moisture control, but their performance depends on a thorough understanding of their chemical, structural, and dynamic properties. Our comprehensive testing service provides the mineralogical, textural, chemical, and dynamic performance insights needed to validate your product, optimise processing parameters, and ensure consistent quality. We combine advanced instrumentation with deep expertise in clay materials to deliver results that are both scientifically rigorous and directly applicable to your quality control and R&D efforts.
We invite you to contact our specialist team to discuss your attapulgite desiccant testing requirements. With our proven track record in industrial mineral characterisation, we are confident we can support your product development, quality assurance, and regulatory compliance goals.
Request your free initial consultation today and discover how our integrated, expert‑led testing services can help you achieve superior moisture management and product reliability.