Reasons for choosing our testing services
ZHONGXI Testing has obtained inspection qualification certifications from multiple countries and regions worldwide. We possess a senior testing team and advanced testing methods, providing independent, impartial, and professional third-party verification services for global carbon projects.
Internationally recognized authority
Certified by multiple international standards such as CNAS, VCS, and GS, with reports universally applicable worldwide.
Global service capability
Covering 140+ countries and regions, it supports on-site detection and remote verification in multiple languages.
Professional experimental methods
Adopt standard experimental methods to ensure accurate and reliable data.
Comprehensive Analytical Testing of Magnetic Bentonite Composites: Advanced Characterisation and Performance Validation
Magnetic bentonite composites—typically synthesised by incorporating superparamagnetic iron oxide nanoparticles (Fe₃O₄ or γ‑Fe₂O₃) onto the layered aluminosilicate structure of bentonite (predominantly montmorillonite)—have emerged as highly efficient and recyclable materials for wastewater treatment, heavy metal immobilisation, organic pollutant adsorption, and catalytic applications. The synergy between bentonite’s high cation exchange capacity (CEC), large specific surface area, and interlayer swelling ability and the rapid magnetic separability of iron oxides enables cost‑effective solid‑liquid separation and reusability. However, the functional performance of these composites is critically governed by magnetic nanoparticle dispersion, preservation of the layered structure, magnetic saturation, surface charge characteristics, and chemical durability under varying pH and ionic conditions. Inhomogeneous loading, pore blockage, or phase transformation can lead to reduced adsorption capacity, slow magnetic recovery, or iron leaching. Our laboratory provides a fully integrated, multi‑scale testing platform specifically engineered for magnetic bentonite materials, combining mineralogical, textural, magnetic, surface chemical, and application‑oriented adsorption assessments. We deliver quantitative, diagnostic, and predictive data that supports material development, process optimisation, quality assurance, and regulatory compliance for environmental, civil engineering, and industrial clients.
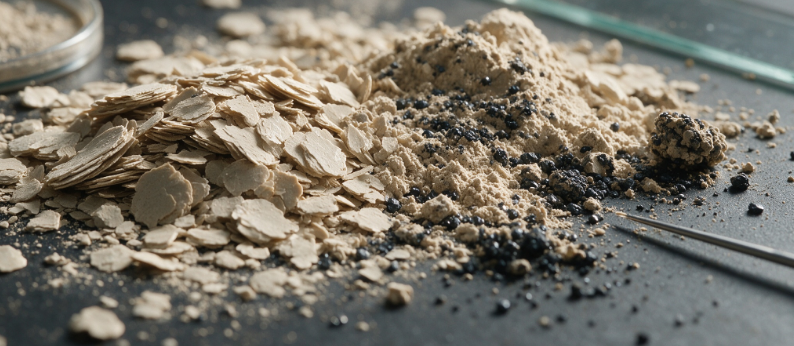
Why Dedicated Testing of Magnetic Bentonite Is Essential for Reliable Environmental and Industrial Applications
Clients seeking testing of magnetic bentonite often encounter challenges such as inconsistent contaminant removal in field trials, incomplete magnetic recovery leading to material loss, or unexpected release of iron into treated water. These issues frequently stem from non‑uniform nanoparticle deposition, inadequate anchoring to the clay layers, or structural collapse during synthesis. Moreover, the chemical stability of the composite in acidic, alkaline, or saline environments must be rigorously verified to prevent dissolution of both the clay matrix and the magnetic phase. Our service provides a systematic characterisation that quantifies specific surface area (BET), cation exchange capacity (CEC), saturation magnetisation (Mₛ), surface hydroxyl density, and adsorption capacity for model pollutants (heavy metals, cationic/organic dyes, phosphates). By identifying the root causes of performance deviations—such as layer exfoliation, magnetic nanoparticle agglomeration, or surface poisoning—we enable clients to optimise synthesis parameters (Fe loading, intercalation method, calcination temperature) and validate batch‑to‑batch consistency for their specific applications.
Our Analytical Capabilities: From Crystal Structure to Magnetic Behaviour and Adsorption Dynamics
Our testing programme is structured into five interconnected modules, each addressing a critical aspect of the composite’s composition, structure, and functional performance:
Mineralogical and microstructural characterisation—We employ powder X‑ray diffraction (PXRD) with Rietveld refinement to identify the montmorillonite basal spacing (001), detect magnetic phases (Fe₃O₄, γ‑Fe₂O₃, or α‑Fe₂O₃), and quantify any amorphous iron‑silicate phases. Fourier‑transform infrared spectroscopy (FTIR‑ATR) and Raman spectroscopy probe Si‑O, Al‑OH, and Fe‑O vibrations, as well as interlayer water and organic modifications. High‑resolution transmission electron microscopy (HR‑TEM) with selected‑area electron diffraction (SAED) and scanning TEM‑EDS mapping visualise the spatial distribution and size of magnetic nanoparticles on the clay layers and within interparticle pores.
Textural and surface area analysis—We determine specific surface area (BET), total pore volume, and pore size distribution (DFT/BJH) using N₂ physisorption at 77 K, covering micro‑ and mesopores. Mercury intrusion porosimetry assesses macroporosity and particle packing. Field‑emission scanning electron microscopy (FE‑SEM) reveals particle morphology, layer stacking, and any delamination. Helium pycnometry measures skeletal density, while cation exchange capacity (CEC) is determined by the ammonium acetate method to quantify the retention of exchange sites after modification.
Magnetic property measurement—We use vibrating sample magnetometry (VSM) and SQUID magnetometry (2–400 K, up to 7 T) to obtain magnetisation hysteresis loops (M‑H), extracting saturation magnetisation (Mₛ), coercivity (H꜀), remanence, and blocking temperature. We also conduct zero‑field‑cooled (ZFC) and field‑cooled (FC) measurements to assess superparamagnetic behaviour. Magnetic separation kinetics are quantified under a defined magnetic field (0.3‑1 T) by monitoring turbidity or particle concentration over time, providing the time to 95 % recovery—a critical parameter for process design.
Surface chemistry and functional group quantification—We characterise surface hydroxyl density via potentiometric titration, and Boehm titration for acidic/basic sites. X‑ray photoelectron spectroscopy (XPS) with depth profiling provides the oxidation states of iron (Fe²⁺/Fe³⁺), the chemical environment of Si, Al, and O, and the binding of magnetic nanoparticles to the clay surface. Zeta potential measurements as a function of pH (2–12) and ionic strength determine the isoelectric point and surface charge behaviour, critical for predicting electrostatic interactions with ionic pollutants.
Adsorption performance, stability, and leachability—We perform batch equilibrium experiments using representative contaminants: heavy metals (Pb²⁺, Cd²⁺, Cu²⁺, As³⁺/As⁵⁺), cationic dyes (methylene blue, malachite green), and anionic species (phosphate, chromate) at environmentally relevant concentrations. We generate adsorption isotherms (Langmuir, Freundlich, Sips) and kinetic profiles (pseudo‑first‑order, pseudo‑second‑order, intraparticle diffusion) under controlled pH (3–10), temperature (10–50 °C), and background electrolyte. We determine maximum adsorption capacity (Qₘ), distribution coefficient (Kd), and selectivity in the presence of competing ions (Ca²⁺, Mg²⁺, SO₄²⁻). Reusability is tested over multiple adsorption‑desorption cycles, while chemical stability is assessed by exposing the composite to acidic (pH 2‑4), alkaline (pH 10‑12), and saline (0.1‑1 M NaCl) conditions for up to 7 days, followed by re‑measurement of BET, XRD, CEC, and Mₛ. Leaching of Fe, Al, and Si into simulated environmental media is quantified by ICP‑MS and ICP‑OES over time.
High‑Level Diagnostic and Predictive Modelling
We integrate adsorption data with surface complexation models (e.g., diffuse‑layer or triple‑layer) to predict pH‑dependent metal binding, and with ion‑exchange equilibrium models to simulate multi‑component adsorption. For column applications, we apply advection‑dispersion‑reaction (ADR) simulations to generate breakthrough curves and design treatment units. Using multivariate statistical analysis (PCA, PLS), we correlate synthesis parameters (Fe/clay ratio, mixing time, drying temperature) with final performance metrics, enabling quality‑by‑design (QbD) optimisation. For failure analysis, we combine post‑use characterisation (XRD, XPS, BET, CEC) with performance history to differentiate between interlayer collapse, magnetic phase oxidation, surface site blocking, or clay dissolution as degradation mechanisms.
Regulatory Compliance and Quality Assurance
All test methods align with ASTM D4646 (CEC), D5757 (adsorbent performance), ISO 9277 (BET), and relevant EPA methods for water quality. Our laboratory holds ISO/IEC 17025:2017 accreditation for a broad scope of materials characterisation and environmental analysis. We provide certified test reports with full measurement uncertainty, traceability to NIST standards, and quality control data (reference materials, blanks, duplicates). For product certification and environmental safety, we support OECD guidelines for ecotoxicity and fate studies.
Our Distinctive Advantages in Magnetic Bentonite Testing
Integrated multi‑technique correlation: We perform all critical analyses on identical sample aliquots, enabling direct correlation between mineralogy (XRD), texture (BET), magnetic properties (VSM), and adsorption capacity (Qₘ). This holistic approach eliminates inter‑batch variability and provides robust structure‑property‑performance relationships.
Realistic environmental simulation: Our adsorption tests use synthetic groundwaters, industrial effluents, and natural organic matter‑containing matrices with controlled competing ions, ensuring that our capacity and selectivity data directly reflect field conditions, not idealised lab water.
Advanced iron speciation and leachate profiling: With Mössbauer spectroscopy (available on request) and high‑resolution XPS, we precisely determine iron oxidation states and magnetic phase composition, and correlate with leaching risks. Our HRMS‑ICP‑MS capability enables detection of trace organic and inorganic leachables, including siloxanes and heavy metals, at sub‑ppb levels.
Expert guidance for material optimisation: Our team includes clay mineralogists, magnetic materials specialists, and environmental engineers who provide specific, actionable recommendations—for instance, optimising the Fe/bentonite ratio to maximise magnetic separability without sacrificing CEC, or suggesting pillaring agents to enhance structural stability in acidic media.
Fast turnaround and flexible sample requirements: Our standard full characterisation package is delivered within 10–14 working days, with expedited 72‑hour service for critical parameters (BET, Mₛ, CEC, and initial adsorption capacity). We handle powders, pellets, and slurries with sample masses as low as 5 g.
End‑to‑End Service Workflow
We initiate each project with a complimentary technical consultation to define your composite composition, target contaminants, application conditions, and performance criteria. We design a customised test plan, advising on sample handling and shipping (including inert atmosphere for oxidation‑sensitive materials). Upon sample receipt, we perform receipt inspection and preconditioning (drying, degassing). All tests are executed with strict QA/QC—reference standards, blanks, and replicate measurements. Data are integrated and reviewed by our lead scientist, then compiled into a comprehensive report containing XRD patterns, TEM/SEM images, BET tables, CEC values, magnetic hysteresis loops, adsorption isotherms, leachate profiles, and a clear executive summary with optimisation recommendations. A post‑report meeting is offered to discuss findings and plan further development or scale‑up steps.
Partner with Us for Reliable, High‑Performance Magnetic Bentonite Solutions
Magnetic bentonite composites offer a cost‑effective and sustainable platform for adsorption and separation, but their success hinges on thorough, multi‑dimensional characterisation. Our testing service provides the scientific rigor, practical relevance, and regulatory support necessary to ensure your material performs reliably in real‑world applications. We have assisted environmental technology firms, water treatment plants, and civil engineering companies in developing and qualifying magnetic bentonite products for market deployment.
We invite you to contact our technical experts to discuss your specific magnetic bentonite testing requirements—whether for product development, batch release, or troubleshooting. With our advanced analytical instruments, accredited protocols, and deep domain expertise, we provide the insights you need to perfect your magnetic bentonite technology and achieve your performance goals with confidence. Request a detailed proposal or schedule a technical consultation today and take the next step towards superior, data‑driven magnetic bentonite solutions.