Reasons for choosing our testing services
ZHONGXI Testing has obtained inspection qualification certifications from multiple countries and regions worldwide. We possess a senior testing team and advanced testing methods, providing independent, impartial, and professional third-party verification services for global carbon projects.
Internationally recognized authority
Certified by multiple international standards such as CNAS, VCS, and GS, with reports universally applicable worldwide.
Global service capability
Covering 140+ countries and regions, it supports on-site detection and remote verification in multiple languages.
Professional experimental methods
Adopt standard experimental methods to ensure accurate and reliable data.
Advanced Performance Testing of Dimethyl Ether (DME) Catalysts: Comprehensive Characterisation and Process Optimisation
Dimethyl ether (DME) catalysts—primarily solid acid catalysts such as γ‑Al₂O₃, zeolites (ZSM‑5, Y, mordenite), and composite catalysts for one‑step synthesis from syngas—are pivotal in the production of a clean fuel and chemical intermediate. The catalytic performance in terms of activity, selectivity to DME, and resistance to deactivation is governed by a delicate interplay of acid site density and strength, pore architecture, hydrothermal stability, and the distribution of active components in bifunctional systems. Even minor variations in synthesis or ageing can lead to reduced conversion, unwanted by‑products (hydrocarbons, CO₂), or rapid coking, significantly impacting process economics. Our laboratory offers a fully integrated, multi‑scale testing platform specifically designed for the rigorous characterisation of DME catalysts, combining advanced physicochemical characterisation, high‑pressure fixed‑bed and slurry‑phase activity testing, kinetic modelling, and accelerated deactivation/regeneration studies. We deliver quantitative, diagnostic, and predictive data that supports catalyst development, quality assurance, process optimisation, and troubleshooting for the chemical, energy, and petrochemical industries.
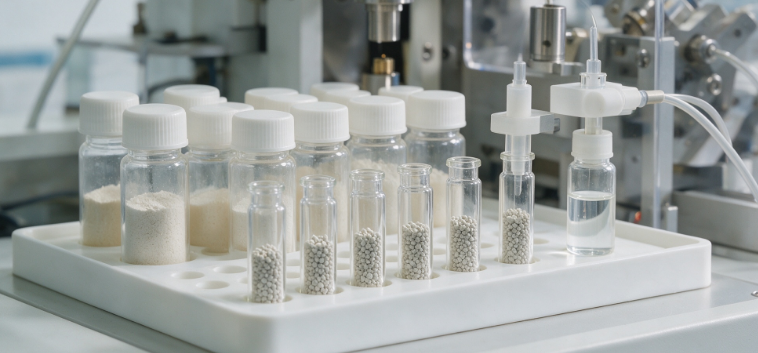
Why Dedicated Testing of DME Catalysts Is Critical for Process Efficiency and Product Quality
Clients seeking DME catalyst testing frequently encounter challenges such as unexpectedly low methanol conversion, poor DME selectivity due to excessive dehydration to hydrocarbons, or rapid catalyst deactivation under industrial operating conditions. These issues often stem from sub‑optimal acidity (too weak or too strong), inappropriate pore size that limits diffusion of reactants/products, or metal poisoning (e.g., sulfur, iron) affecting the bi‑functional components. Moreover, the effect of water, CO₂, and feed impurities on catalyst stability is often underestimated without realistic long‑term testing. Our service provides a systematic evaluation that quantifies methanol conversion, DME selectivity, by‑product distribution (olefins, paraffins, CO₂), coke formation kinetics, and catalyst lifetime under simulated industrial conditions (temperature, pressure, space velocity, feed composition). By identifying the root causes of performance deficits—such as acid site loss, pore blockage, or phase transformation—we enable clients to optimise catalyst formulation, adjust operating conditions, and implement effective regeneration protocols for reliable and cost‑efficient DME production.
Our Analytical Capabilities: From Crystal Structure and Acidity to Dynamic Reactor Performance and Durability
Our testing framework is structured into five interconnected modules, each addressing a critical dimension of DME catalyst behaviour:
Structural and chemical characterisation—We determine specific surface area (BET), total pore volume, and pore size distribution (DFT/BJH) via N₂ physisorption at 77 K. X‑ray diffraction (XRD) with Rietveld refinement confirms zeolite framework type, crystallinity, and any impurity phases. X‑ray photoelectron spectroscopy (XPS) and Fourier‑transform infrared spectroscopy (FTIR‑ATR) characterise the chemical states of surface elements and identify any organic or inorganic contaminants. Temperature‑programmed desorption of ammonia (NH₃‑TPD) and pyridine‑adsorbed FTIR quantify total acidity and the distribution of Brønsted and Lewis acid sites, which are critical for DME synthesis. For bi‑functional catalysts, we also perform hydrogen chemisorption and TPR to characterise metal dispersion and reducibility.
Catalytic activity and selectivity testing—We operate continuous flow fixed‑bed reactors and slurry‑phase autoclaves to simulate industrial DME synthesis from methanol dehydration or syngas conversion. Using realistic feed compositions (methanol, H₂/CO/CO₂ ratios), we measure conversion, selectivity to DME, and by‑product formation as functions of temperature (150‑350 °C), pressure (1‑50 bar), weight‑hourly space velocity (WHSV), and time‑on‑stream (TOS). Products are analysed by on‑line gas chromatography (GC‑FID/TCD) with appropriate columns to separate DME, methanol, CO₂, and C₁‑C₅ hydrocarbons. We derive kinetic parameters (activation energy, reaction orders) and provide performance maps to identify the optimal operating window.
Deactivation, regeneration, and coking studies—We conduct accelerated deactivation tests under elevated temperature or with the introduction of model poisons (e.g., water, sulphur compounds, heavy hydrocarbons). Thermogravimetric Analysis (TGA) coupled with mass spectrometry (MS) quantifies coke deposition and characterises its nature (e.g., aliphatic vs. aromatic, hydrogen/carbon ratio). We evaluate regeneration protocols (calcination in air or diluted oxygen) and assess the recovery of activity, selectivity, and structural integrity through multiple cycles. Post‑regeneration characterisation (XRD, BET, NH₃‑TPD) identifies irreversible changes such as dealumination, sintering, or phase transformation.
Hydrothermal and contaminant tolerance testing—We simulate steam treatment at elevated temperatures (up to 600 °C) to assess hydrothermal stability, which is critical for industrial processes with recycled streams. We also evaluate the effect of feed impurities (methanol impurities, sulphur, chlorides) on catalyst activity and selectivity, providing data to set realistic feed pretreatment requirements.
Advanced in‑situ and operando analysis—For mechanistic insight, we offer in‑situ FTIR and Raman spectroscopy under reaction conditions to monitor adsorbed species (e.g., methoxy groups, surface formates) that are intermediates in DME formation. This enables us to link surface chemistry directly with catalytic performance, guiding rational catalyst improvement.
High‑Level Predictive Modelling and Diagnostic Interpretation
We integrate kinetic, characterisation, and deactivation data to build comprehensive kinetic models that describe both the main reaction and side‑reaction pathways. Using multivariate statistical analysis (PCA, PLS), we correlate synthesis parameters (Si/Al ratio, metal loading, calcination temperature) with key performance indicators (activity, selectivity, stability), enabling quality‑by‑design (QbD) optimisation. For post‑mortem diagnostics, we combine post‑use characterisation with operational history to distinguish between coking, acid site neutralisation, and structural collapse as primary deactivation mechanisms, providing actionable guidance for process adjustment or catalyst reformulation.
Regulatory Compliance and Quality Assurance
All test methods are aligned with ASTM, ISO, and industry standards for catalyst characterisation and gas analysis. Our laboratory is ISO/IEC 17025:2017 accredited for a broad scope of physicochemical and catalytic testing. We issue certified test reports with full measurement uncertainty, traceability to NIST/CRM reference materials, and quality control data (reference catalysts, blanks, duplicate runs). For intellectual property and process scale‑up, we provide comprehensive data packages with detailed protocols and raw data archives.
Our Distinctive Advantages in DME Catalyst Testing
Integrated catalyst fingerprinting: We perform XRD, BET, NH₃‑TPD, TGA, and reactor testing on identical sample batches, enabling direct correlation between acidity, pore structure, and catalytic performance. This holistic approach eliminates cross‑sample variability and provides a complete understanding of the catalyst's strengths and weaknesses.
Realistic industrial simulation: Our high‑pressure, high‑temperature rigs allow testing under conditions that closely mimic commercial DME plants, including the presence of recycled gases and water. This ensures that our data are directly scalable and predictive, not just academic.
Advanced coking and regeneration diagnostics: We combine TGA‑MS with in‑situ IR to not only measure coke quantity but also to identify the chemical nature and location of deposits, enabling tailored regeneration strategies that minimise permanent damage.
Expert guidance for plant optimisation: Our team includes chemical engineers with deep experience in DME synthesis. We provide specific, actionable recommendations—for example, adjusting feed temperature to balance conversion and selectivity, or implementing a guard bed to remove sulphur contaminants that rapidly poison the catalyst.
Fast turnaround and flexible sample formats: Our standard characterisation and performance package is delivered within 10‑14 working days, with expedited 72‑hour screening for key parameters (conversion, selectivity, and deactivation trend). We handle powder, extrudate, and pellet catalysts, as well as industrial spent samples.
End‑to‑End Service Workflow
We initiate each project with a complimentary technical consultation to define your catalyst composition, target process (methanol dehydration or syngas‑to‑DME), and performance targets. We design a customised test plan, including handling and shipping guidelines (e.g., inert atmosphere, desiccant). Upon sample receipt, we perform preconditioning (calcination, reduction) and characterisation. All tests are executed with strict QA/QC—reference catalysts, blanks, and duplicates. Data are integrated and reviewed by our lead catalysis scientist, then compiled into a comprehensive report containing characterisation results, kinetic curves, selectivity profiles, deactivation trends, and a clear executive summary with optimisation recommendations. A post‑report meeting is offered to discuss findings and plan further development or plant implementation.
Partner with Us for Reliable, High‑Performance DME Catalyst Solutions
DME is increasingly recognised as a clean fuel and versatile intermediate, but its production economics depend on robust and selective catalysts. Our testing service provides the scientific depth, practical realism, and regulatory support necessary to ensure your catalyst delivers optimal performance over its lifetime. We have supported DME technology developers, catalyst manufacturers, and industrial producers in optimising their catalytic processes.
We invite you to contact our technical experts to discuss your specific testing needs—whether for catalyst screening, quality control, or troubleshooting. With our advanced analytical instruments, accredited protocols, and specialised catalysis expertise, we provide the insights you need to achieve superior DME production. Request a detailed proposal or schedule a technical consultation today and take the next step towards data‑driven catalyst excellence.