Reasons for choosing our testing services
ZHONGXI Testing has obtained inspection qualification certifications from multiple countries and regions worldwide. We possess a senior testing team and advanced testing methods, providing independent, impartial, and professional third-party verification services for global carbon projects.
Internationally recognized authority
Certified by multiple international standards such as CNAS, VCS, and GS, with reports universally applicable worldwide.
Global service capability
Covering 140+ countries and regions, it supports on-site detection and remote verification in multiple languages.
Professional experimental methods
Adopt standard experimental methods to ensure accurate and reliable data.
Comprehensive Diagnostic Testing for Plasma Arc Welding Torches
The plasma arc welding (PAW) torch is a precision electro‑mechanical‑thermal system that generates a constricted, high‑temperature plasma arc for joining metals with exceptional depth‑to‑width ratios and minimal heat‑affected zones. Unlike gas‑tungsten arc welding (GTAW) torches, PAW torches incorporate a secondary gas circuit, a water‑cooled copper nozzle, and a precisely aligned electrode–orifice configuration, all of which must function in concert to sustain a stable, non‑transferred or transferred arc. When clients search for plasma arc welding torch inspection or PAW torch performance verification, they are typically encountering symptoms that threaten weld quality: arc wander, inconsistent keyhole penetration, excessive nozzle wear, or erratic high‑frequency start. The core need is not a superficial visual examination but a systematic, multi‑parametric evaluation that quantifies the torch’s electrical integrity, cooling efficiency, gas flow dynamics, and electrode/nozzle degradation—all correlated to the resulting weld bead geometry. Our testing service delivers this holistic assessment, combining advanced metrology, flow analysis, and simulated welding trials to ensure that your PAW torch operates at its peak capability.
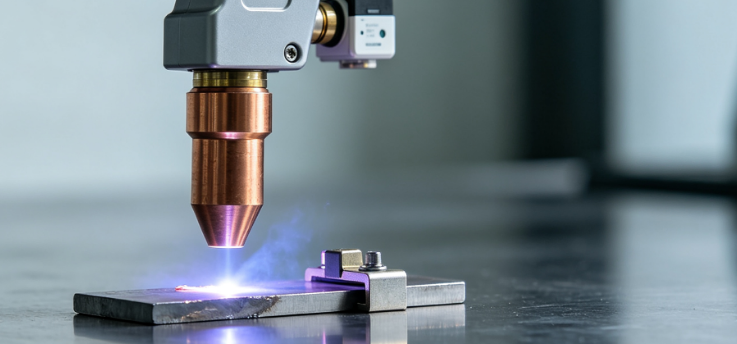
Critical Failure Precursors in Plasma Arc Welding Torches
A PAW torch is subjected to severe operational stresses: arc temperatures exceeding 20 000 K at the nozzle orifice, cooling water pressures up to 8 bar, and continuous exposure to ultraviolet radiation and metal vapour condensation. Over time, these factors induce several failure modes. The tungsten electrode undergoes sputtering and evaporation, altering its tip geometry and thereby shifting the arc attachment point. The copper nozzle experiences erosion from ion bombardment, leading to orifice enlargement and loss of arc constriction—directly reducing plasma jet velocity and heat flux density. Simultaneously, internal O‑ring seals can degrade under thermal cycling, causing gas or coolant leakage that destabilises the arc or risks water ingress into the weld zone. Additionally, the electrical insulation between the electrode and the nozzle can develop carbon tracking or moisture absorption, creating parasitic Leakage Currents that affect the pilot arc transfer. Conventional workshop checks—such as electrode concentricity or coolant flow observation—capture only a fraction of these potential issues. Our diagnostic approach addresses each of these failure pathways with dedicated, high‑resolution measurements.
Our Integrated Testing Protocol for PAW Torches
We have structured our torch testing into four complementary modules, each designed to isolate a specific performance domain while also cross‑correlating data for a unified health assessment.
Module 1 – Electrical Characterisation and Insulation Integrity: Using a hipot tester with variable DC and AC voltages (up to 5 kV), we measure the Insulation Resistance between the electrode, nozzle, body, and cooling water circuit under controlled temperature and humidity. We simultaneously perform a capacitance‑frequency sweep (10 Hz to 1 MHz) to detect any dielectric losses or incipient tracking that could compromise the high‑frequency start circuit. Our system detects Leakage Currents as low as 0.5 µA, well below the threshold that would cause intermittent arc ignition failures.
Module 2 – Gas Flow Dynamics and Pressure Drop Analysis: We connect the torch to a mass‑flow controlled test bench that replicates the actual gas supply (Ar, He, H₂ mixtures) at pressures from 0.5 to 10 bar. We measure the volumetric flow rate vs. pressure differential across the torch body, including the primary plasma gas and secondary shielding gas circuits. By applying a transient pressure‑decay method, we calculate the effective flow resistance and detect any partial blockages or internal leakage paths. Our proprietary flow‑distribution mapping uses a miniature pressure scanner to compare the exit velocities from multiple discrete gas ports, identifying asymmetries that could lead to arc deflection.
Module 3 – Coolant Circuit Performance and Thermal Imaging: We circulate a temperature‑controlled water/glycol mixture through the torch while monitoring the pressure drop and flow rate with ultrasonic flowmeters (accuracy ±0.5 %). At the same time, we apply a simulated heat load using an external resistance heater to replicate the thermal input from the arc. High‑resolution infrared thermography captures the surface temperature distribution of the torch body, revealing any hot spots caused by blocked coolant passages or poor heat transfer due to scale deposition. Our analysis quantifies the thermal resistance of the cooling path and compares it to the torch’s design specifications, providing a clear margin to over‑heating.
Module 4 – Electrode and Nozzle Micro‑metrology: After removing the consumable parts, we employ a non‑contact coordinate measuring system (based on chromatic confocal sensing) to map the electrode tip radius, concentricity, and surface roughness. For the nozzle, we measure the orifice diameter (to ±1 µm) and examine the bore surface with a digital microscope and scanning electron microscopy (SEM) if needed, to identify micro‑cracks or molten metal spatter adhesion. These dimensional data are compared with a baseline reference to determine the remaining service life of each component under the user’s typical operating current.
Advanced Diagnostics: Dynamic Arc Behaviour Simulation
To bridge the gap between static measurements and real‑world welding performance, we have developed a captive‑torch test station that allows us to actually strike and sustain a pilot arc (or transferred arc) on a water‑cooled copper anode under controlled conditions. During this test, we capture high‑speed video (up to 10 000 fps) of the arc root attachment on the electrode and the orifice exit. Concurrently, we record the voltage and current waveforms at a sampling rate of 2 MHz, enabling us to compute the arc resistance, dynamic impedance, and the flicker noise power spectral density. These dynamic signatures are highly sensitive to electrode wear and nozzle constriction. For example, an increase in low‑frequency noise (0.1–10 Hz) often correlates with electrode tip roughening, while a rise in high‑frequency noise (>1 kHz) indicates flow turbulence or spatter. Our proprietary algorithm, ArcHealth™, extracts a set of dimensionless metrics from these waveforms and ranks the torch’s condition relative to a comprehensive database of new and degraded torches. This provides a quantitative, repeatable “performance score” that supplements the physical inspection data.
Our Distinctive Competencies in PAW Torch Testing
Our service stands out through a combination of specialised instrumentation, deep process knowledge, and flexible service models. Unlike general calibration laboratories, we maintain a dedicated plasma‑welding laboratory staffed by certified welding engineers (IWE) and plasma physicists who understand the nuances of keyhole mode, melt‑in mode, and pulsed‑arc welding. We have tested torches from all major manufacturers (including Thermal Dynamics, ESAB, Lincoln Electric, and Soudronic) and custom‑built systems for aerospace and nuclear applications. Our ISO/IEC 17025 accreditation covers electrical safety, flow measurement, and dimensional metrology, ensuring traceability to international standards.
We also offer on‑site testing services for torches that are difficult to transport, using a portable version of our test rig that can be set up in your workshop. This includes the same flow, coolant, and electrical checks, supplemented by a handheld thermal camera and a borescope for internal inspection. Our turnaround time for a full laboratory test suite (including the dynamic arc test) is 5‑7 working days, while the on‑site basic check can be completed within 4 hours. All reports are issued in a structured PDF format with clear pass/fail criteria, trend graphs, and proactive maintenance suggestions—such as electrode re‑grinding schedules, nozzle replacement intervals, and coolant filter change recommendations.
Interpretive Reporting and Corrective Guidance
We believe that testing without interpretation is merely data collection. Therefore, our final report includes a root‑cause analysis section that links any out‑of‑spec measurement to its likely operational consequence. For instance, a 2 % reduction in primary gas flow due to a partially blocked swirl ring will be translated into an expected 5‑10 % decrease in arc stiffness, leading to wider weld beads. We then propose specific corrective actions—whether it is cleaning the gas filter, replacing O‑rings, or adjusting the electrode setback. Where appropriate, we also provide updated process parameters (e.g., a slightly higher flow rate or lower current) to compensate for minor degradation until scheduled maintenance can be performed. This consultative approach has been particularly valued by clients who rely on PAW for critical applications such as tube‑to‑tubesheet welding in heat exchangers, where even minor torch variations can cause costly rework.
Validation Through Field Performance Correlation
Over the past five years, we have assessed over 300 PAW torches across various industries. Our internal database allows us to benchmark a given torch against its peers of similar age and usage profile. In one case, a heavy‑equipment manufacturer was experiencing frequent high‑frequency start failures on a robotic PAW cell. Our insulation and capacitance testing revealed that the ceramic insulator had absorbed moisture due to a cracked cooling hose fitting—a defect that was invisible to visual inspection. After drying and resealing, the start reliability returned to 99.8 %. In another instance, a tube mill noticed a gradual increase in blowholes; our flow‑distribution mapping identified an asymmetric wear pattern in the secondary gas ring, which was corrected by a simple re‑centring of the gas distributor. These examples underscore the tangible benefits of moving beyond “visual and go/no‑go” checks to a comprehensive diagnostic philosophy.
Engaging Our Plasma Arc Welding Torch Testing Services
We invite clients to schedule a preliminary consultation to define the scope of testing tailored to your torch type, usage history, and quality requirements. Whether you need a one‑time health check, periodic condition monitoring, or a forensic investigation after a weld defect, we will propose a customised test plan with a fixed price and a delivery schedule. For urgent cases, we maintain a priority service with results available in 48 hours for laboratory tests. After each engagement, we provide ongoing technical support to help you implement our recommendations and track the improvement in weld quality.
Contact our PAW torch diagnostics team to initiate a discussion. With our state‑of‑the‑art measurement systems, validated arc‑behaviour simulation, and application‑oriented reporting, we ensure that your plasma arc welding torch operates at its maximum capability—delivering consistent, defect‑free welds that meet the most demanding quality standards.